
The Bottleneck Nobody Sees (Until It Burns You)
Last April, a thunderstorm parked over the Brooklyn Navy Yard while my crew prepped a same-day run for a pop-up line. In that mess, our dtf printer had to move 180 PET film sheets in under four hours—would your setup eat that clock without smears, do-overs, or refunds? I’ve been buying, speccing, and running print gear for over 15 years on the B2B side, and I’ve learned the real fight isn’t color; it’s time. We run an a2 dtf printer daily because the sheet area and feed stability change how we plan shifts, not just how we hit tones. If your turnaround windows are tight, your villains are sneaky: RIP software waits, white ink circulation hiccups, and a powder shaker that can’t stay in step with your print pace (yo, that lag racks up quick). I’ve watched a 12% scrap rate vanish overnight just by syncing film feed and cure time—same art, same staff, different clock.
Traditional workarounds look clean on paper but fold under pressure. Pre-coating film too far ahead leads to humidity bites; batching jobs by color sounds smart but starves your queue when white underbase needs more dwell; swapping roll-to-sheet mid-run kills momentum at the worst hour. That’s where an A2 bed and dialed platen alignment matter—the print area reduces swaps, and the film path stays predictable, so your curing oven doesn’t play roulette with hand-offs. The hidden pain isn’t “speed.” It’s sync: can the printer cadence, shaker rhythm, and cure profile stay locked when the PO lands after lunch and the truck leaves at six? I treat timing like rent—miss it once, and you’re paying double next month. Let’s zoom in on why the next move has to be different, not louder.
Forward Moves: Build a Schedule That Prints Back
What’s Next
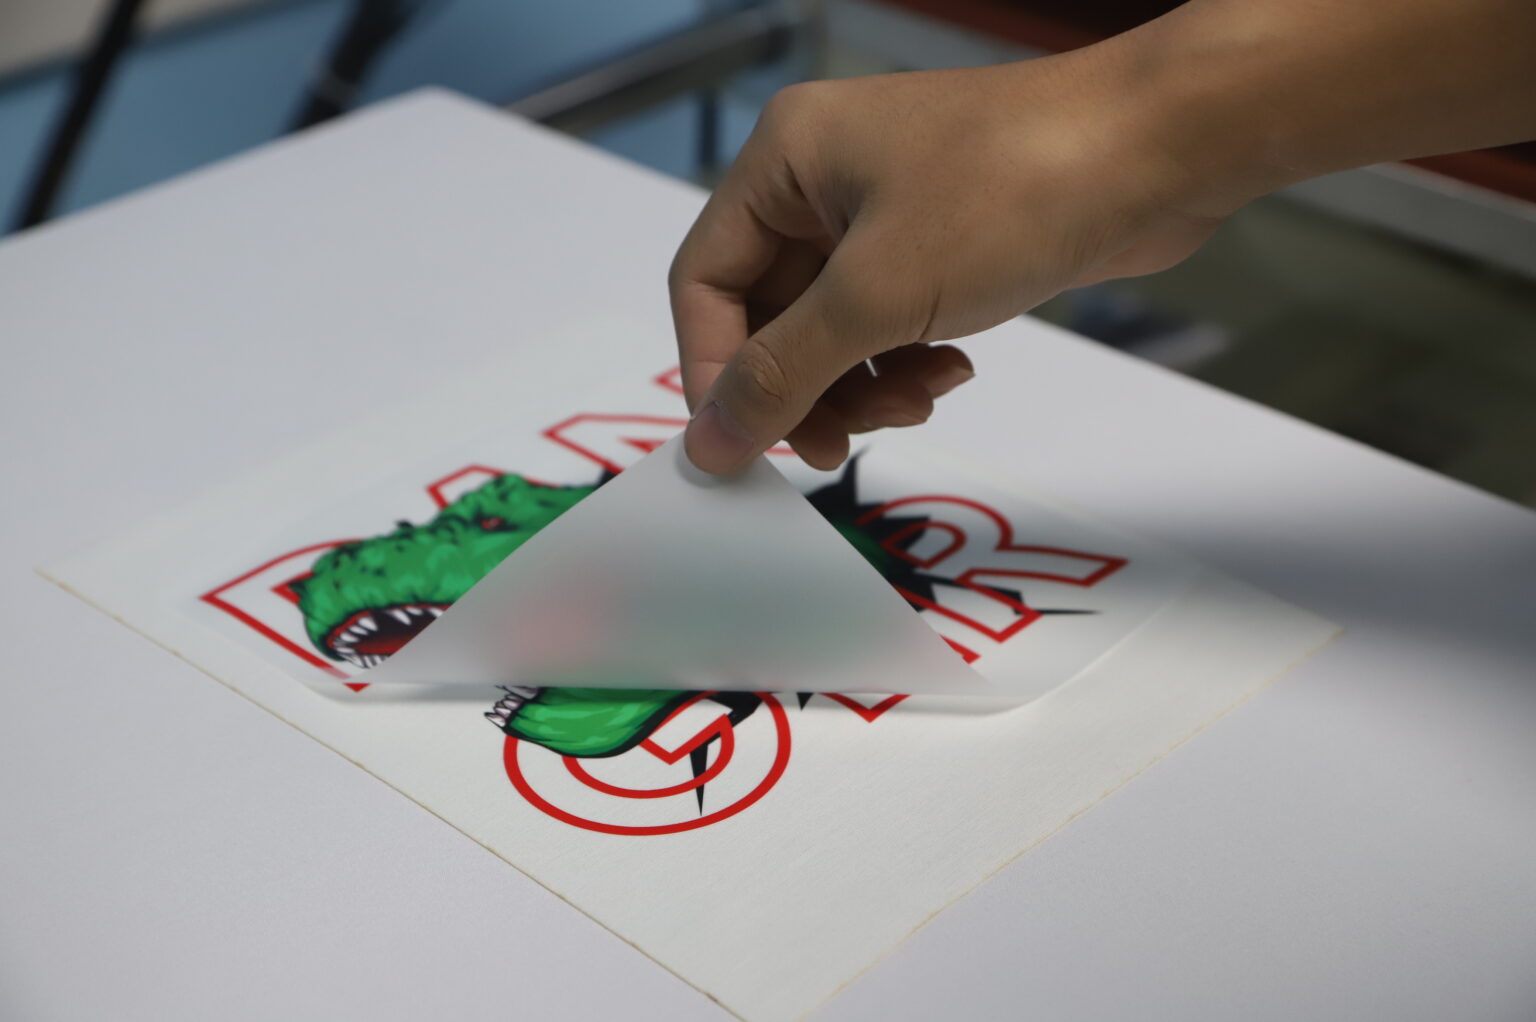
Let’s get technical, but keep it plain. Throughput is a chain—print pass → powder coat → cure. Break one link, and the whole shop drags. An A3 rig can hit nice samples, sure, but it cycles shorter sheets and begs for more handling, which invites banding and powder clumps when the room gets sticky. An a2 dtf printer shifts the math: larger sheets mean fewer starts and stops, steadier white ink layers, and less babysitting of ICC profiles when you push saturation. Hold up—none of that matters if your powder shaker can’t match your printer’s linear meters per hour. I match shaker capacity to the printer’s real-world output, not brochure speed, and I time the cure window to the thickest white pass, not the “average” one. Result: fewer cracked transfers, no mystery clog hunts at 3 a.m., and consistent press temps across tees and nylon windbreakers.
Comparatively, older workflows rely on operators to “feel” the dwell time. That’s cute until a rainy day adds five minutes to the dry and your queue implodes. Better route: lock process to numbers and repeat them. Track warm-up variance for your heads, log circulation intervals for white ink, and cap queue length by powder throughput—not wishful thinking. I deadass switched a client in Midtown from rolling singles to ganged A2 layouts last summer; they cut handling touches by 37% and stopped chasing micro-banding from rushed reloads. If you’re evaluating options, I suggest three metrics that don’t lie: 1) cross-device sync—does printer speed match shaker and cure capacity under peak load; 2) downtime index—how often does white ink circulation pause you per 8-hour shift; 3) scrap-to-ship ratio—what percent of films miss on cure or powder because the line drifted. Keep it real, keep it measured, and you’ll ship the heat, not headaches—and keep your rep tight with buyers who need their drops on time. Xinflying