
Opening — the one problem that keeps coming back
I’ve been folding conveyor belts and redrawing plant grids for decades, and one truth won’t quit: a fancy robot can’t hide a bad plan. When I first started comparing shop-floor sketches to real output, I kept finding the same mismatch between intent and reality. That gap is where manufacturing automation technology can help, but only if you pair it with sensible decisions about flow and capacity. I watched practical demos of technology Integration solutions at The Battery Show North America and left thinking the problems are always the same — just dressed differently.

Problem: layout that betrays throughput
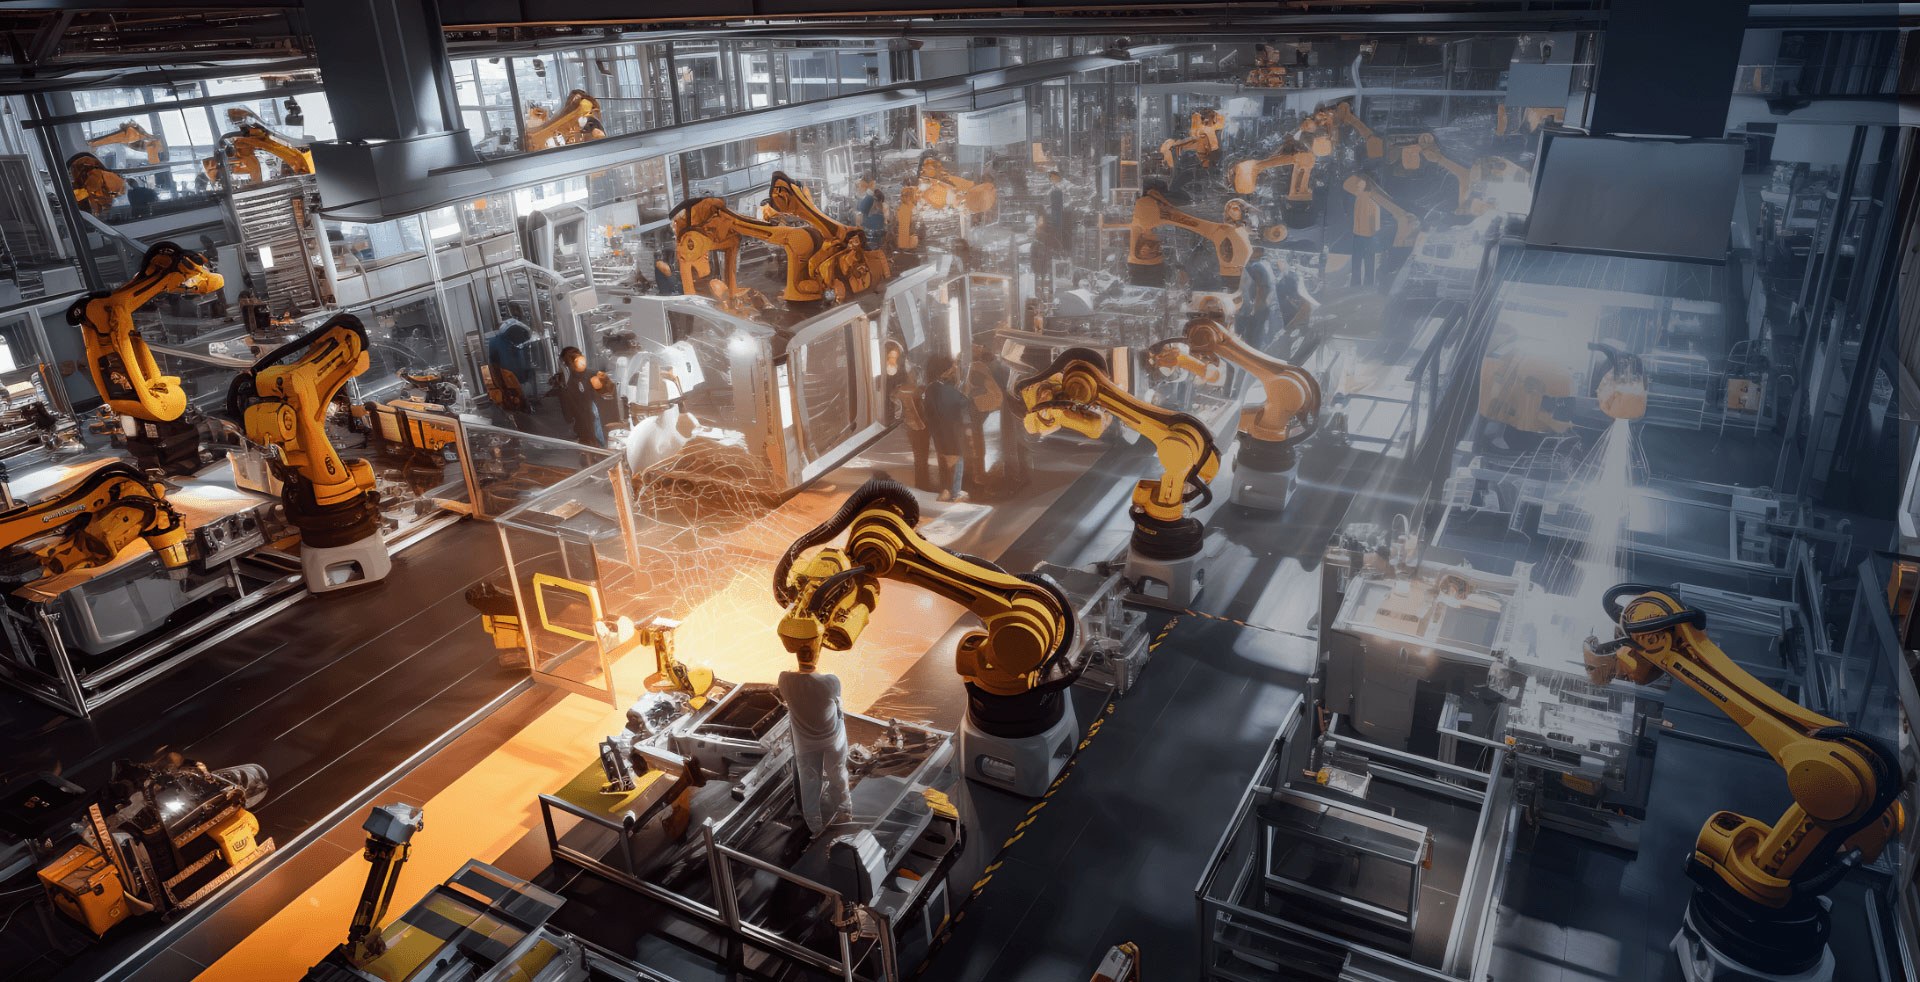
Plants are often drawn by people who like tidy lines, not by the people who have to thread cells through test stands. Common missteps I see:- Long travel routes that multiply handling time.- Mixed process zones where fast and slow operations collide.- Insufficient buffer space causing cascading stoppages.Fix these and the robot arms do what they’re supposed to: raise consistent throughput instead of masking chaos.
Problem: capacity assumptions that don’t match process reality
Managers quote takt times from specs. Technicians watch machines hiccup. The root causes are simple:- Ignoring tool changeover time.- Not counting inline quality checks.- Assuming each station operates at rated uptime.Check these with real cycle-timestamping for a week. You’ll find the single bottleneck that limits overall output.
Layout principles that actually hold up
Years on the floor taught me a handful of rules that beat fancy spreadsheets:- Design for a clear process sequence first; pack equipment second.- Place buffers where variable process steps meet fixed-rate lines.- Keep maintenance access and part kitting within one operator reach.Make a paper mockup and walk it with operators before you spend on conveyors.
Process requirements: controls, quality, and repeatability
Battery assembly tolerances and cell handling demand control systems that log and react. My practical checklist:- Closed-loop control for temperature and torque where it matters.- Traceability from cell ID to pack assembly.- Inline electrical and leakage tests, not only final acceptance.Automation needs data gates, not just motion. If you can’t reproduce a failure from logs, you won’t fix it.
When to centralize control and when to decentralize
Central PLC rooms look neat on diagrams, but decentralization sometimes reduces wiring cost and single-point failure risk. Think in terms of failure modes:- Centralized: easier coordinated recipes, simpler software updates.- Decentralized: local resilience, shorter cable runs, less downtime from a single controller fault.Decide based on the number of stations that must act simultaneously and how often you expect to change production recipes.
Integration choices — what vendors don’t always tell you
You’re choosing not just conveyors and robots but the glue that makes them talk. Expect these trade-offs:- Off-the-shelf MES modules speed start-up but limit customized quality logic.- Custom integration lets you catch rare failure modes but costs more during commissioning.- Prefer modular integration layers so cell-testers and pack-assembly stations can be swapped without rewiring the whole line.Ask for run-to-failure scenarios from any integrator and verify their error logs. That single test separates polished integrations from overpromised ones.
Common pitfalls and how to avoid them
I’ve seen promising projects stall for predictable reasons:- Skipping operator input during design — they know where the shortcuts are.- Under-budgeting for commissioning and iterations.- Treating software as an afterthought.Avoid these by reserving at least 15–20% of the project time for on-floor trials and by keeping an integration plan that lists data points you need for diagnostics.
Vendor comparison: practical criteria
When weighing suppliers, use objective checks, not marketing gloss:- How do they log error conditions? Ask to see example logs.- Can they deliver a rollback to a previous recipe safely?- Do they provide documented maintenance recipes for consumables?Score suppliers on those items and you’ll get a clearer ranking than feature lists give.
Final thoughts — what actually delivers value
After years of retrofits and fresh installs, the projects that last are the ones where layout, realistic capacity planning, and clear process rules were decided first, then automation chosen to support them. That’s practical work: hiring people who know the floor, testing assumptions with live runs, and insisting on integration that makes faults visible. When those pieces fit, the line behaves as promised — and that’s the outcome I expect from partners like FHS.